


发那科BHC宏程序——CNC螺栓孔圆自定义刀具
提交者:cnc programmer
图纸/图像
CNC程序
/*Parameters
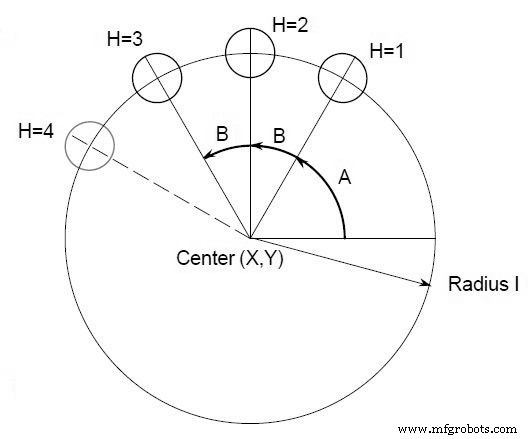
G65 P9100 Xx Yy Zz Rr Ff Ii Aa Bb Hh
X: X coordinate of the center of the circle (#24)
Y: Y coordinate of the center of the circle (#25)
Z: Hole depth (#26)
R: Coordinates of an approach point (#18)
F: Cutting feedrate (#9)
I: Radius of the circle (#4)
A: Drilling start angle (#1)
B: Incremental angle (Clockwise when negative value) (#2)
H: Number of holes (#11)
*/
O9100
#3=#4003
G81 Z#26 R#18 F#9 K0
IF[#3 EQ 90]GOTO 1
#24=#5001+#24
#25=#5002+#25
N1
WHILE[#11 GT 0]DO 1
#5=#24+#4*COS[#1]
#6=#25+#4*SIN[#1]
G90 X#5 Y#6
#1=#1+#2
#11=#11-1
END 1
G#3
G80
M99
/*Fanuc Bolt Hole Macro Example
Example macro call to drill 5 holes at intervals of 45 degrees after a start angle of 0 degrees on the circumference of a circle with radius 4". The absolute center of the circle is (10", 5").
*/
O0002
G90 G92 X0 Y0 Z4.0
G65 P9100 X10.0 Y5.0 R1.0 Z-2.0 F20 I4.0 A0 B45.0 H5
M30
数控机床
- 双发那科机器人改造升级 Precision Cup Denester,大幅提升效率
- 专业定制 CNC 加工解决方案——精准可靠
- 精密CNC加工定制零件:快速、精准、量身定制的解决方案
- 定制激光雕刻节日礼物:提升品牌记忆点
- CNC G72 螺栓孔角度排布编程:精准钻削实例代码
- Haas CNC G71 螺栓孔圆弧排布:高效圆弧阵列钻削实例
- Fanuc G68 坐标旋转:精准轴对齐的 CNC 编程详解
- 精通 Fanuc G04 停留命令:CNC 精准计时控制
- Fanuc G04 暂停命令详解: 掌握数控加工中的延时控制
- 使用 Fanuc 宏程序和 G66 模态调用创建自定义 G81 钻削循环
- Alpha X 系列车床采用定制控制系统,性能卓越
- FANUC CNC 系统变量命名引用:让自定义宏更易读、易维护