


高级 G65 宏:CNC 铣削精确半径增量编程
提交者:Machinist
工程图/图片
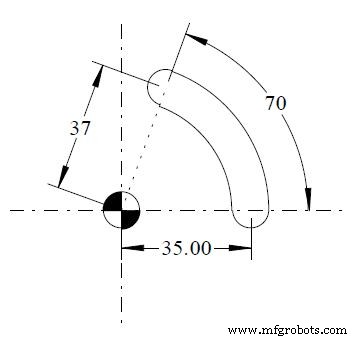
CNC 程序
;A = #1 (Start Angle 0 degrees) ;B = #2 (Start Radius) ;C = #3 (Increment angle for accuracy calculations.) ;I = #4 (Finish Angle) ;J = #5 (Finish radius) ;K = #6 (Milling feed) O2222 T5 M6 G0 G90 G40 G21 G17 G94 G80 G54 X35 Y0 S500 M3 G43 Z100 H? Z5 G1 Z-0.5 F200 G65 P8999 A0 B35 C0.01 I70 J37 K500 G0 G90 Z100 M30 O8999 #7 = #4 / #3 ;1) Total no. of moves 70 / 0.01 #8 = [[#5 - #2] / #7] ;2) Increase in radius 37-35/7000 N1 #2 = #2 + #8 ;3) Next Radius i.e. 35+inc. radius. #1 = #1 + #3 ;4) Increase in angle #9 = #2 * COS [ #1 ] ;5) New X axis position #10 = #2 * SIN [ #1 ] ;6) New Y axis position G1 X#9 Y#10 F#6 ;7) Feed move to new positions ;8) If new angle is less than finish angle go to line N1. IF [#1 LT #4] GOTO 1 G0 Z10 M99
该程序展示了一个螺旋线/渐开线型刀路的宏程序 O8999,通过 G65 P8999 调用。参数:起始角度 A=0,起始半径 B=35,角度增量 C=0.01°,终止角度 I=70°,终止半径 J=37,进给 K=500。宏内计算总步数 #7,每步半径增量 #8,然后在循环 N1 中累加角度与半径,计算新的 X、Y 坐标并插补。适用于螺旋铣削、渐开线轮廓等变半径曲线加工。
数控机床