


G65 宏程序:精准内椭圆加工
提交者:Machinist
工程图/图片
CNC 程序
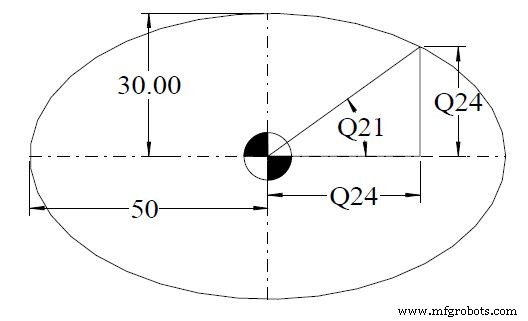
T1 M6 G0 G90 G40 G21 G17 G94 G80 G54 X0 Y0 S? M3 G43 Z5 H? G1 Z-? F? #20 = 2 ; Incremental degree calculation #21 = 0 ; Start Angle #22 = 30 ; Y Axis Radius #23 = 50 ; X Axis Radius G41 X#23 D? ; Compensation motion to right side of internal pocket N10 #21 = [#21 + #20] ; Angular Count #24 = SIN[#21] ; Incremental Y axis calculation #25 = COS[#21] ; Incremental X axis calculation #24 = [#24*#22] ; Absolute Y calculation #25 = [#25*#23] ; Absolute X calculation X#25 Y#24 ; Movement in X & Y axis IF [#21 LT 360] GOTO 10 ; Restart if less than 360 degree motion IF [#21 GT 360] GOTO 20 ; If final angle becomes greater than 360 degrees recalculate IF [#21 EQ 360] GOTO 30 ; Finish if total angle is equal to 360 degree N20 #21 = 360 GOTO 10 N30 G40 X0 G0 G90 Z100 M30
该宏程序利用 G65 调用(此处为主程序内嵌宏逻辑),通过三角函数计算椭圆上的点位,实现内椭圆轮廓铣削。变量 #22、#23 分别为 Y、X 轴半径,#20 为角度增量(2°)。循环通过正弦/余弦计算 X、Y 坐标,配合 G41 刀具半径补偿加工内部轮廓。程序包含角度边界判断,确保闭合 360°。实际使用需设置主轴转速 S、进给 F、刀具长度补偿 H、刀具半径补偿 D 等参数。
数控机床